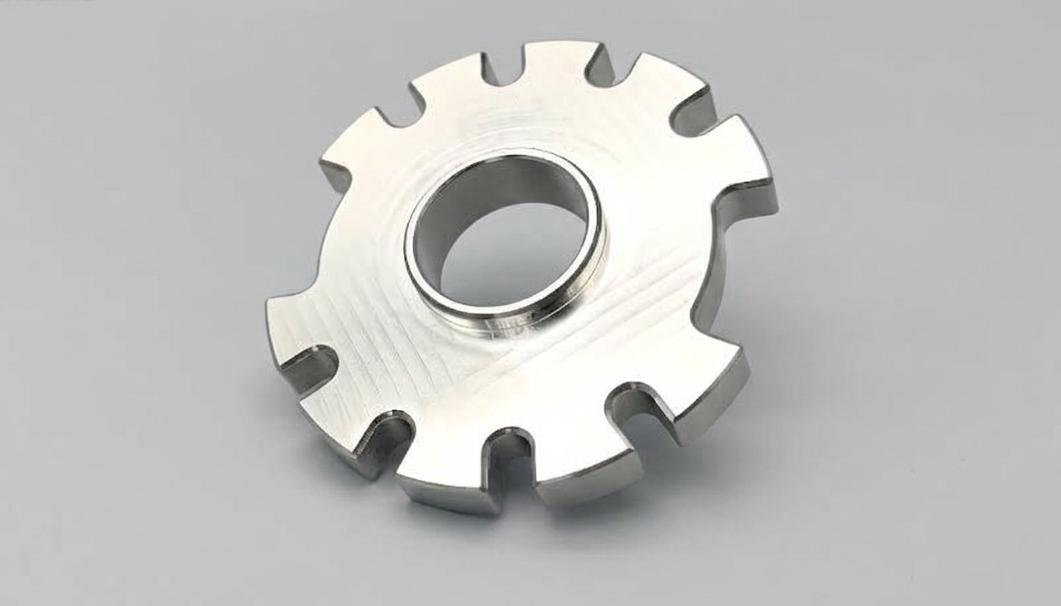
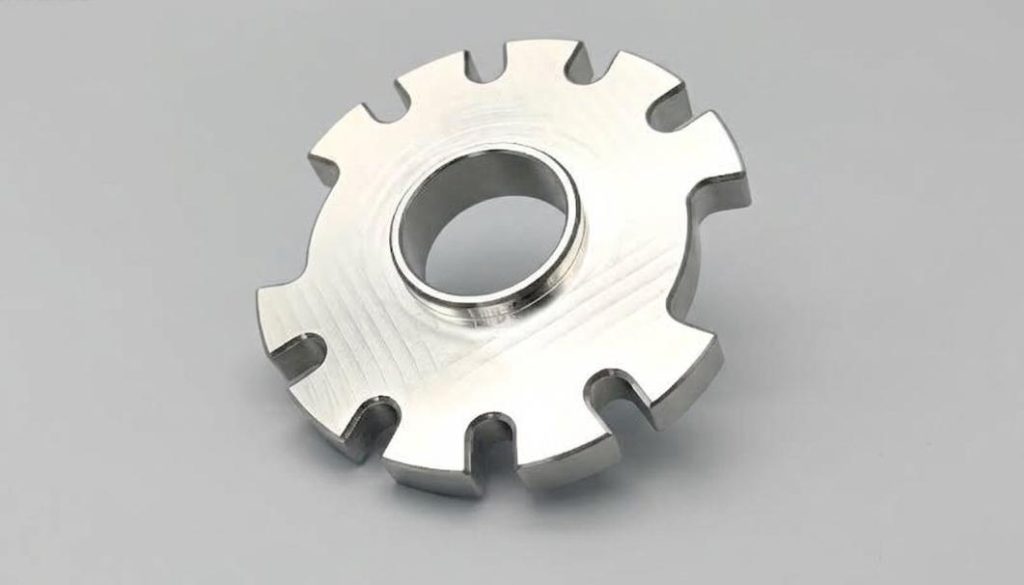
CNC machined Aluminum Toothed Disc
- Material: AL 6061-T6
- Size: None
- Process: CNC Machining
- Surface treatment: None
This aluminum toothed disc is produced through a combined turning and milling process. Bar stock is first machined on a CNC lathe to form the outer diameter, bore, and central hub, then transferred to a machining centre for milling the evenly distributed peripheral slots. The part is deburred after machining. Anodizing can be applied on request.
Machining Challenges
High indexing accuracy required across all evenly distributed slots. The peripheral slots must be spaced at perfectly equal angular intervals around the disc. Any deviation in one slot’s index position affects the functional symmetry of the entire disc. This kind of consistent equal-division accuracy can’t be left to operator judgment — it needs a process method that enforces it systematically.
Cutter breakage risk at slot root corners. When the milling cutter reaches the bottom corner of each slot, the cutting force direction changes abruptly. That sudden load transition is exactly where tool breakage concentrates. A broken cutter in this position not only loses the tool — it typically damages the slot floor in a way that’s difficult to recover through any subsequent operation.
Coaxiality risk when transferring between turning and milling setups. After turning is complete, the part must be moved to the machining centre for slot milling. The datum reference changes between the two setups, and any misalignment between them results in the milled slot centres being offset from the turned bore centre — a coaxiality error that directly affects how the part assembles and functions.
How It’s Managed
| Stage | Approach |
| Indexing accuracy | 4th-axis rotary table used for slot indexing — equal division controlled by the CNC controller, eliminating the error accumulation of manual indexing |
| Datum consistency | Reference faces established in a single turning setup before any milling begins, giving the milling process a stable, consistent datum that minimizes inter-setup positional shift |
| Tooling selection | Sharp aluminium-specific cutters with a small-radius arc toolpath at slot floors — distributes the load through the corner transition rather than concentrating it at a single point |
| Process sequencing | Turning and milling operations sequenced and fixtured to minimize repeat positioning error between setups, keeping slot positions coaxial with the bore within the required tolerance |