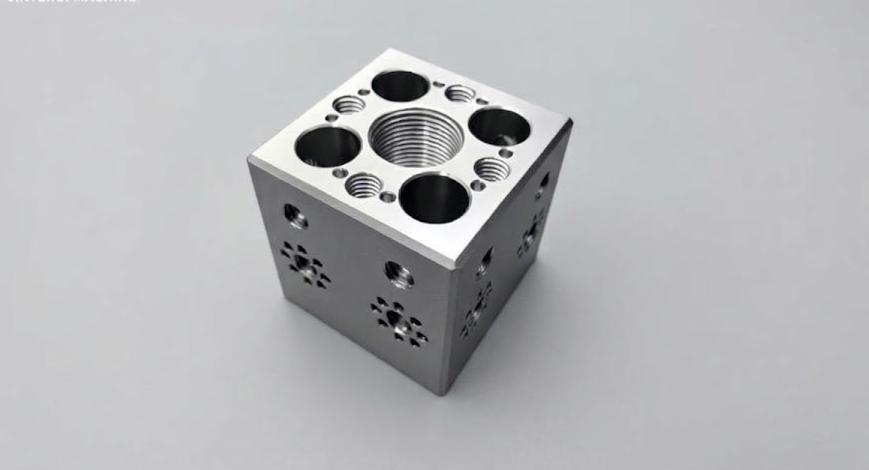
CNC Machined Cube-Style Multi-Face Reference Block
- Material: AL6061
- Size: D27.9X41.7 mm
- Process: CNC Machining
- Surface treatment: Clear Anodizing
This is a cube-style reference block with hole patterns on multiple faces, which can also serve as a hydraulic manifold block. It is a cube-shaped body with through holes, counterbores, and tapped holes on all six faces and a large threaded hole in the center, and the hole patterns on different faces intersect each other. It is machined on a CNC machining center in several flips and finished to a clean natural surface.
Hole position, squareness between faces, and the accuracy of hole intersections are all tightly controlled. The block can work as a fixture reference module or as a fluid distribution manifold.
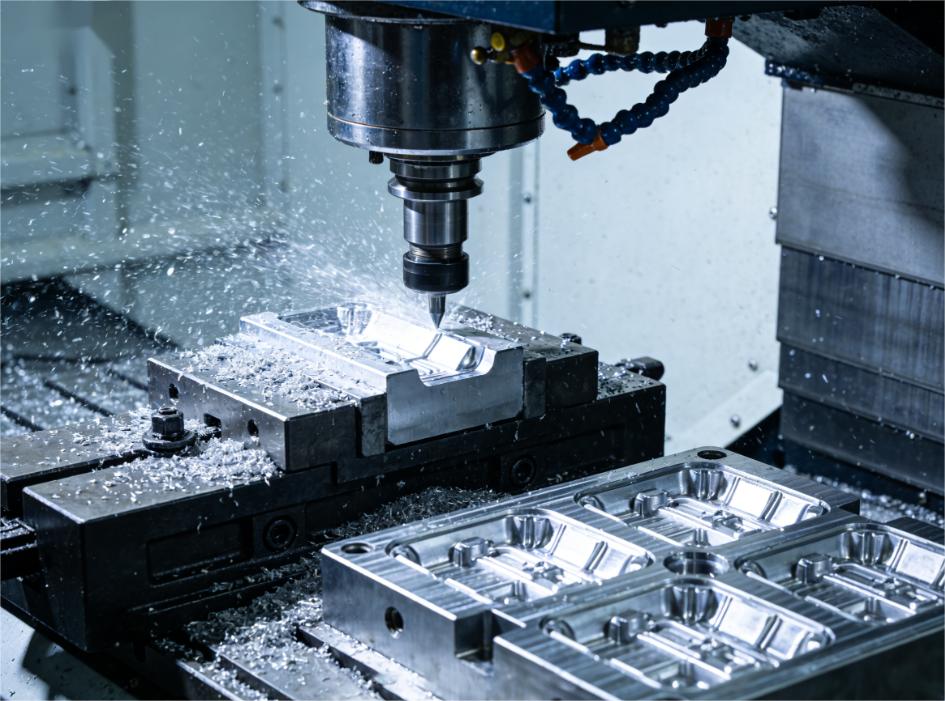
Machining Challenges
- Holes on six faces, with intersecting hole patterns. Cross-drilled holes can break into each other, drift off position, or interfere when drilling through.
- Squareness and flatness across all faces must be high. Flipping and re-clamping repeatedly builds up positioning error.
- Deep threads, large holes, and small holes are mixed together. Tapping can wander or break the tap, and burrs at hole entries are hard to control.
- Deburring internal cross holes is difficult. Remaining burrs can restrict fluid flow or interfere with assembly.
- Wall thickness is uneven. Cutting stress can distort the block and ruin datum face accuracy.
How It’s Managed
| Issue | Approach |
| Accumulated flip error | Precision fixturing, with the datum re-indicated at every flip and geometric tolerances tightly controlled |
| Hole pattern interference | Operations sequenced as small holes first, then enlarging larger holes, finishing the bores before tapping, to avoid interference between holes |
| Cross-hole burrs | A dedicated deburring process for cross holes to clear burrs at the intersections |
| Internal stress and distortion | Stock left on after roughing and stress relief performed before finishing the datum faces and hole patterns |
| Inspection | Flatness, squareness, and hole position checked on a CMM, with threads verified using go/no-go gauges |